 English
 中文版
Advantages of IH Chemical Pump
From:YangTze River Time:2026/10/8 16:59:24
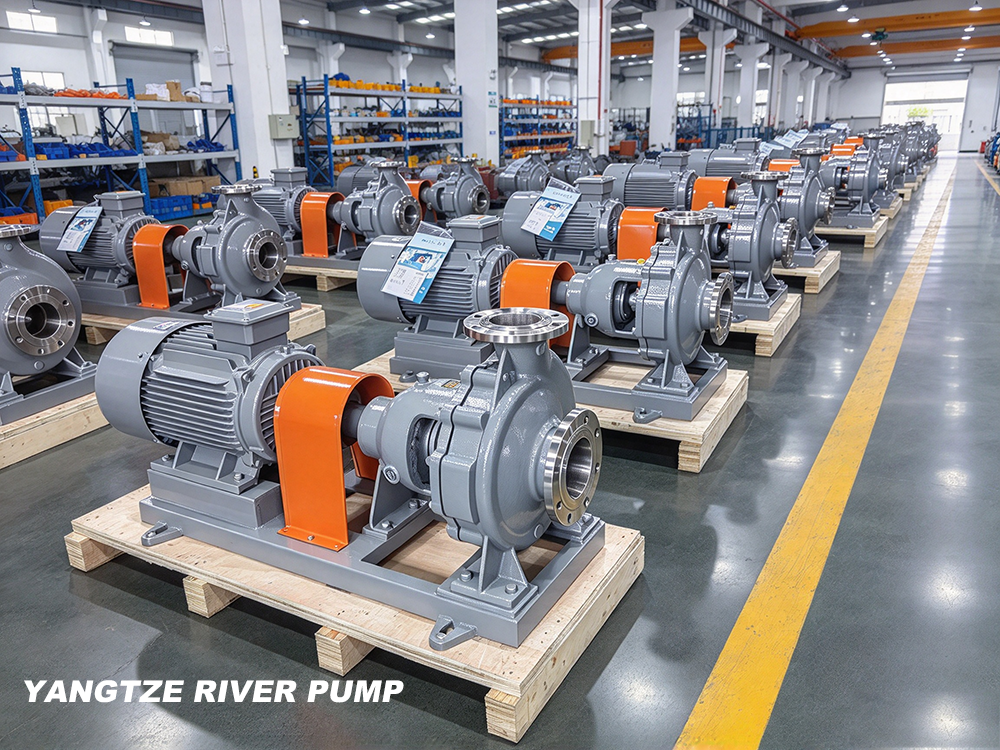
The IH chemical pump is a single-stage, single-suction horizontal centrifugal pump complying with ISO2858 international standards. It is a mainstream fluid transfer equipment widely used in chemical, environmental protection, pharmaceutical, printing and dyeing industries. Compared with traditional old-style chemical pumps, it has outstanding advantages in performance, energy consumption, maintenance and safety. It can perfectly meet working conditions for conveying various corrosive liquids and serves as the preferred industrial fluid transfer equipment. Its specific advantages are as follows:
 1. High efficiency and energy saving with good economic performance
Adopting an optimized advanced hydraulic model, the IH chemical pump delivers excellent hydraulic performance. Its efficiency is much higher than that of traditional chemical pumps, achieving remarkable energy-saving effects. Long-term continuous operation effectively cuts power consumption for enterprises. Besides, it features good anti-cavitation performance, hardly suffering cavitation damage during operation, stable energy consumption and no extra energy loss, suitable for long uninterrupted production.
2. Strong corrosion resistance for diverse working conditions
The wetted parts can be made of anti-corrosion materials such as 304 and 316L stainless steel, which can stably convey weak acid, weak alkali, salt solution and other corrosive media without erosion. It has a wide applicable temperature range: normally from -20℃ to 105℃. With cooling sealing structure, it can withstand media temperature up to 280℃ to satisfy temperature and medium requirements of different chemical processes.
3. Reasonable structure for convenient maintenance
Equipped with classic back pull-out design, there is no need to disassemble pipelines or move the motor during overhaul and parts replacement. Only the pump cover assembly needs to be detached to take out internal components like impeller and seals for repair and replacement, greatly shortening downtime and reducing maintenance difficulty and labor cost. Standardized and highly interchangeable parts make spare parts procurement easy and lower long-term maintenance cost.
4. Reliable sealing to eliminate leakage risks
This pump supports packing seal, single / double mechanical seal and other sealing types, which can be flexibly selected according to medium characteristics and working conditions. With special flushing and cooling auxiliary schemes, stable sealing prevents leakage of corrosive media, avoids material loss, environmental pollution and equipment corrosion, ensuring safe, clean and compliant workshop production.
5. Stable operation and long service life
The main shaft is protected by a special shaft sleeve to isolate corrosive media. Matched with high-precision stable bearing bracket, the pump runs with low vibration, low noise and low failure rate. It has a long continuous operation cycle and rarely breaks down, adapting to continuous and large-scale production in chemical industry, with better durability than traditional pumps.
6. Wide versatility and easy installation
Compact, small and lightweight, the IH chemical pump is easy to install with flexible pipeline layout. Complete series specifications cover a wide range of flow and head. High standardization and interchangeability enable quick matching for new project supporting or replacement of old equipment, with broad application scenarios.
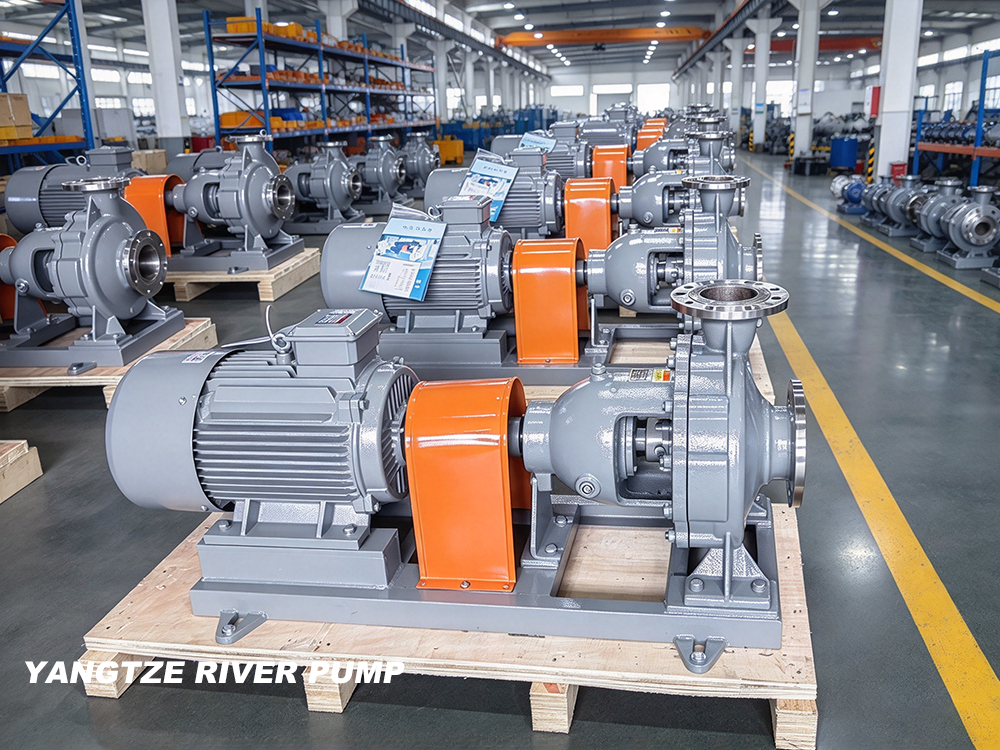 In summary, with core strengths including high efficiency & energy saving, corrosion resistance, easy maintenance, stable safety and wide adaptability, the IH chemical pump overcomes the drawbacks of traditional chemical pumps. It can effectively reduce enterprise production and operation costs and guarantee stable and efficient operation of industrial fluid transfer processes, making it an ideal equipment for conveying corrosive media in chemical, environmental protection, pharmaceutical, electroplating and many other industries.
Adopting an optimized advanced hydraulic model, the IH chemical pump delivers excellent hydraulic performance. Its efficiency is much higher than that of traditional chemical pumps, achieving remarkable energy-saving effects. Long-term continuous operation effectively cuts power consumption for enterprises. Besides, it features good anti-cavitation performance, hardly suffering cavitation damage during operation, stable energy consumption and no extra energy loss, suitable for long uninterrupted production.
2. Strong corrosion resistance for diverse working conditions
The wetted parts can be made of anti-corrosion materials such as 304 and 316L stainless steel, which can stably convey weak acid, weak alkali, salt solution and other corrosive media without erosion. It has a wide applicable temperature range: normally from -20℃ to 105℃. With cooling sealing structure, it can withstand media temperature up to 280℃ to satisfy temperature and medium requirements of different chemical processes.
3. Reasonable structure for convenient maintenance
Equipped with classic back pull-out design, there is no need to disassemble pipelines or move the motor during overhaul and parts replacement. Only the pump cover assembly needs to be detached to take out internal components like impeller and seals for repair and replacement, greatly shortening downtime and reducing maintenance difficulty and labor cost. Standardized and highly interchangeable parts make spare parts procurement easy and lower long-term maintenance cost.
4. Reliable sealing to eliminate leakage risks
This pump supports packing seal, single / double mechanical seal and other sealing types, which can be flexibly selected according to medium characteristics and working conditions. With special flushing and cooling auxiliary schemes, stable sealing prevents leakage of corrosive media, avoids material loss, environmental pollution and equipment corrosion, ensuring safe, clean and compliant workshop production.
5. Stable operation and long service life
The main shaft is protected by a special shaft sleeve to isolate corrosive media. Matched with high-precision stable bearing bracket, the pump runs with low vibration, low noise and low failure rate. It has a long continuous operation cycle and rarely breaks down, adapting to continuous and large-scale production in chemical industry, with better durability than traditional pumps.
6. Wide versatility and easy installation
Compact, small and lightweight, the IH chemical pump is easy to install with flexible pipeline layout. Complete series specifications cover a wide range of flow and head. High standardization and interchangeability enable quick matching for new project supporting or replacement of old equipment, with broad application scenarios.

